
LOCTITE EA 901NA-B1
Harmonization Code : 5906100000 | Adhesive tape of a width not exceeding 20cm
Main features
- Thixotropic Gap-Filling Control
- 50-Minute Working Window
- Room-Temperature Application Cure
Product Description
LOCTITE EA 901NA-B1 is a two-component, room-temperature-curing epoxy paste adhesive for bonding metals, rubber, plastics, wood and glass. The gray Part A and amber Part B change to red during thorough mixing, providing a visible mixing indicator. Its thixotropic, sag-resistant paste consistency supports controlled placement and gap filling on bonding surfaces. A 100:23 mix ratio by weight provides a 50-minute pot life for a 450 g mass at 25°C. Assemblies reach handling strength in 8 hours at 25°C, with full cure available through a five-day room-temperature schedule or an accelerated one-hour cure at 93°C. Fully cured bonds resist water, salt spray and most organic liquids.
Key features
- Thixotropic epoxy paste: Sag-resistant rheology helps the mixed adhesive remain in place and supports gap filling.
- Visible mixing indicator: Gray and amber components change to red as the two parts are thoroughly mixed.
- Controlled working window: Typical pot life is 50 minutes for a 450 g mass at 25°C.
- Flexible cure options: Cure for five days at 25°C or accelerate cure with one hour at 93°C.
- Environmental exposure resistance: Fully cured bonds resist water, salt spray and most organic liquids.
Applications / Suitable for
- Bonding prepared metal substrates, including aluminum and steel
- Plastic-to-metal and engineering-plastic bonding
- Bonding rubber, wood and glass where the joint design and surface preparation are validated
TDS, SDS & Technical Documents
Technical Specifications
Physical Properties
General Properties
Additional Information
LOCTITE EA 901NA-B1
This two-component, thixotropic epoxy paste adhesive bonds metals, rubber, plastics, wood and glass. It cures at room temperature, changes from gray and amber components to red during thorough mixing, and provides sag-resistant placement on bonding surfaces. The system supports gap filling and reaches handling strength in 8 hours at 25°C, with room-temperature and accelerated heat-cure options.

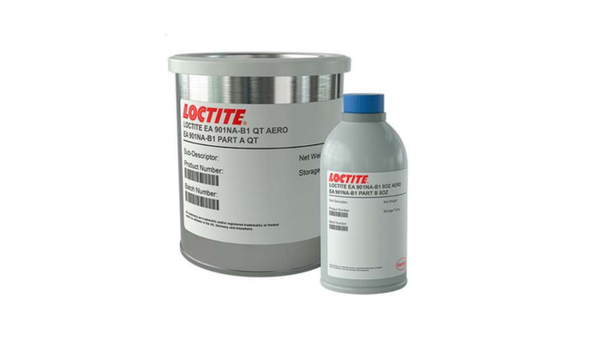
LOCTITE EA 901NA-B1 two-component adhesive system.
As-supplied component properties
| Property | Value | Unit | Method / condition |
|---|---|---|---|
| Part A color | Gray | - | As supplied |
| Part B color | Amber | - | As supplied |
| Part A viscosity | 530 | Pa·s | Brookfield HBT, spindle 7 at 2.09 rad/s, 25°C |
| Part B viscosity | 3.0 | Pa·s | Brookfield HBT, spindle 1 at 2.09 rad/s, 25°C |
| Part A shelf life | 1 | year | Store below 4°C (40°F) |
| Part B shelf life | 1 | year | Store below 4°C (40°F) |
Mixing, application and cure
Bring both components close to room temperature, mix at the specified weight ratio, and apply to clean, dry, properly prepared surfaces. Control mixed batch size because the reaction generates heat.
Bonding sequence
Store both components below 4°C (40°F) for a one-year shelf life. Ambient shipment does not alter the standard warranty when the material is placed into its intended storage upon receipt. Use adequate ventilation, avoid skin and eye contact, and review the current component labels and safety information before handling.
Cured bulk material properties
| Property | Value | Unit | Method / condition |
|---|---|---|---|
| Tensile strength | 29.6 | MPa | ASTM D638; 3.18 mm castings; tested at 25°C |
| Tensile modulus | 540 ksi (approximately 3.72 GPa) | - | ASTM D638; 3.18 mm castings; tested at 25°C |
| Elongation at break | 0.9 | % | ASTM D638; 3.18 mm castings; tested at 25°C |
| Shore D hardness | 90 | - | Tested at 25°C |
| Compressive strength | 122.6 | MPa | ASTM D695; 12.7 mm castings; cured 24 hours at 25°C and tested at 25°C |
Typical tensile lap-shear strength by cure and test temperature
Typical laboratory results for phosphoric-acid-anodized 2024-T3 Alclad aluminum. Values are specific to the stated substrate, surface preparation, cure schedule, test temperature and ASTM D1002 configuration.
| Property | Value | Unit | Method / condition |
|---|---|---|---|
| Tensile lap shear at -55°C | 12.4 | MPa | ASTM D1002; cured 24 hours at 25°C; 2024-T3 Alclad aluminum, phosphoric-acid anodized per ASTM D3933 |
| Tensile lap shear at -55°C | 23.4 | MPa | ASTM D1002; cured 1 hour at 93°C; 2024-T3 Alclad aluminum, phosphoric-acid anodized per ASTM D3933 |
| Tensile lap shear at 25°C | 19.3 | MPa | ASTM D1002; cured 24 hours at 25°C; 2024-T3 Alclad aluminum, phosphoric-acid anodized per ASTM D3933 |
| Tensile lap shear at 25°C | 24.1 | MPa | ASTM D1002; cured 1 hour at 93°C; 2024-T3 Alclad aluminum, phosphoric-acid anodized per ASTM D3933 |
| Tensile lap shear at 66°C | 7.6 | MPa | ASTM D1002; cured 24 hours at 25°C; 2024-T3 Alclad aluminum, phosphoric-acid anodized per ASTM D3933 |
| Tensile lap shear at 66°C | 23.4 | MPa | ASTM D1002; cured 1 hour at 93°C; 2024-T3 Alclad aluminum, phosphoric-acid anodized per ASTM D3933 |
| Tensile lap shear at 93°C | 4.8 | MPa | ASTM D1002; cured 24 hours at 25°C; 2024-T3 Alclad aluminum, phosphoric-acid anodized per ASTM D3933 |
| Tensile lap shear at 93°C | 17.2 | MPa | ASTM D1002; cured 1 hour at 93°C; 2024-T3 Alclad aluminum, phosphoric-acid anodized per ASTM D3933 |
| Tensile lap shear at 121°C | 4.8 | MPa | ASTM D1002; cured 1 hour at 93°C; 2024-T3 Alclad aluminum, phosphoric-acid anodized per ASTM D3933 |
Additional performance evidence
Environmental, substrate and temperature results support product evaluation when the complete test configuration is considered.
Bonding applications and substrate contexts
Evaluate the adhesive with the intended substrate grade, surface preparation, joint design, cure schedule and service exposure.


Aerospace structural adhesive selection guide
Discuss LOCTITE EA 901NA-B1 for your bonding process
Contact Krayden to discuss substrate preparation, mix and cure options, bondline requirements, product availability, and the evaluation conditions most relevant to your aerospace or industrial assembly.


