
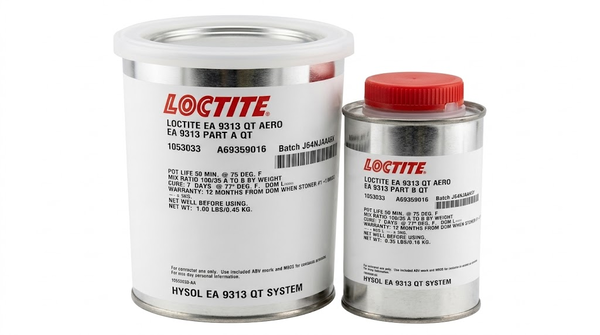
LOCTITE EA 9313
Harmonization Code : 3506.91.90.99 | Prepared glues and other prepared adhesives, not elsewhere specified or included; products suitable for use as glues or adhesives, put up for retail sale as glues or adhesives, not exceeding a net weight of 1 kg ; Adhesives based on polymers of headings 3901 to 3913 or on rubber; Other ; Other
Main features
- Flexible Cured Adhesive
- 0.6 to 1.5 Pa s Mixed Viscosity
- 60-Minute Working Window
Product Description
LOCTITE EA 9313 AERO is a two-component epoxy paste adhesive formulated for flexible bonds in aerospace and industrial assemblies. Its mixed viscosity of 0.6–1.5 Pa·s at 25°C provides a pourable consistency that can be injected into preassembled parts, while the cured adhesive supports bonding between dissimilar substrates. The system cures at room temperature and provides a 60-minute pot life at 25°C. Typical performance on phosphoric-acid-anodized 2024-T3 AlClad aluminum includes 31.0 MPa tensile lap shear and 267 N/25 mm floating-roller peel at 25°C after a five-day room-temperature cure. The product may also be used as a laminating resin and for potting small assemblies.
Key features
- Flexible cured bondline: Supports bonded joints where substrate dissimilarity and peel loading are important evaluation factors.
- Pourable mixed viscosity: 0.6–1.5 Pa·s at 25°C supports injection into preassembled parts.
- Room-temperature cure: Develops normal performance after five days above 25°C, with accelerated cure options for small adhesive masses.
- Controlled processing window: 60-minute pot life at 25°C for a 200 g mixed mass.
- Mechanical performance: Typical lap shear reaches 31.0 MPa at 25°C and 28.9 MPa at −55°C on the tested anodized aluminum configuration.
Applications / Suitable for
- Bonding dissimilar substrates
- Injection bonding of preassembled parts
- Laminating resin applications
- Potting small assemblies
TDS, SDS & Technical Documents
Technical Specifications
General Properties
Physical Properties
Additional Information
LOCTITE EA 9313 AERO
A two-component, room-temperature-curing epoxy paste with a pourable mixed viscosity and a flexible cured bondline. The adhesive is suited to bonds requiring peel strength and low-temperature performance, including joints between dissimilar substrates, and it can be injected into preassembled parts.

LOCTITE EA 9313 AERO two-component epoxy paste adhesive.
As-Supplied Properties
| Property | Value | Unit | Method / condition |
|---|---|---|---|
| Part A color | Off-white | — | As supplied |
| Part B color | Red | — | As supplied |
| Mixed color | Pink | — | Immediately after mixing |
| Part A viscosity | 13–24 (130–240) | Pa·s (P) | 25°C; Brookfield HBT, spindle 3 at 20 rpm |
| Part B viscosity | 0.025–0.045 (0.25–0.45) | Pa·s (P) | 25°C; Brookfield HBT, spindle 1 at 100 rpm |
| Mixed viscosity | 0.6–1.5 (6–15) | Pa·s (P) | 25°C; Brookfield LVF, spindle 1 at 60 rpm |
| Part A density | 1.11 | g/mL | As supplied |
| Part B density | 1.01 | g/mL | As supplied |
| Mixed density | 1.09 | g/mL | Mixed system |
| Peak exotherm | 188 at 70 minutes | °C | 250 g mass; ASTM D2471 water-bath method |
Processing and Cure
Use the specified component ratio, control mixed batch size, and maintain contact between the parts through the handling-strength stage. Cure time can be shortened by increasing temperature within the stated limits.
Store Parts A and B between 0°C and 25°C in closed containers. Shelf life is 1 year below 25°C for each component. Part A may crystallize at 4°C or below; restore it by heating Part A to 49°C for 1–2 hours, cooling to ambient temperature, and hand-mixing with a spatula before combining with Part B. Keep the separate components near room temperature before mixing.
Cured Material Properties
Typical bulk-resin properties. These values describe cured test specimens and are not bonded-joint design allowables.
| Property | Value | Unit | Method / condition |
|---|---|---|---|
| Tensile strength | 45 | MPa | 25°C; 3.18 mm castings; ASTM D638 |
| Tensile modulus | 2,274 | MPa | 25°C; 3.18 mm castings; ASTM D638 |
| Elongation at break | 8.0 | % | 25°C; 3.18 mm castings; ASTM D638 |
| Shore D hardness | 80 | — | 25°C; cured bulk resin |
| Glass transition temperature | 49 | °C | Cured bulk resin |
| Shear modulus, dry | 889 | MPa | 25°C; cured bulk resin |
| Poisson’s ratio | 0.36 | — | Cured bulk resin |
| Compressive strength | 62.3 | MPa | 25°C; 12.7 mm castings; ASTM D695 |
| Compressive modulus | 1,812 | MPa | 25°C; 12.7 mm castings; ASTM D695 |
| Dielectric constant | 3.86 | — | 1 kHz and 25°C; ASTM D150 |
| Dissipation factor | 0.012 | — | 1 kHz and 25°C; ASTM D150 |
Bond Performance
Typical bond data are specific to the stated aluminum substrate, surface preparation, cure, and test methods.
| Test temperature | Typical value | Unit | Method |
|---|---|---|---|
| −55°C | 28.9 | MPa | ASTM D1002 |
| 25°C | 31.0 | MPa | ASTM D1002 |
| 60°C | 6.2 | MPa | ASTM D1002 |
| 71°C | 4.1 | MPa | ASTM D1002 |
Applications
The product can be evaluated for flexible bonding and low-viscosity application tasks supported by the specified mix and cure process.


Evaluate LOCTITE EA 9313 AERO for your bonding process
Contact Krayden to discuss substrate preparation, mixing and cure conditions, batch-size controls, handling strength, or performance data for your assembly.


