
LOCTITE EA 9323
Harmonization Code : 3506.91.90.99 | Prepared glues and other prepared adhesives, not elsewhere specified or included; products suitable for use as glues or adhesives, put up for retail sale as glues or adhesives, not exceeding a net weight of 1 kg ; Adhesives based on polymers of headings 3901 to 3913 or on rubber; Other ; Other
Main features
- Low-Viscosity Adhesive Application
- 30-Minute Working Window
- 5-Day Cure Cycle
Product Description
LOCTITE EA 9323 AERO is a two-component, low-viscosity epoxy paste adhesive for room-temperature repair of metal and composite aerospace structures. The unfilled amber system supports laminating and injection processes and combines a 30-minute pot life at 25°C for a 450 g mass with handling strength after 24 hours and full room-temperature cure in 5 to 7 days. Typical tensile lap shear reaches 28.9 MPa at 25°C on phosphoric-acid-anodized 2024-T3 AlClad aluminum after a 5-day cure. The adhesive also retains 7.6 MPa at 121°C under the same ASTM D1002 configuration, providing high-temperature strength data for application evaluation.
Key features
- Two-component epoxy paste: Amber Part A and Part B form an unfilled structural adhesive system.
- Low-viscosity components: Part A is 170 Pa·s and Part B is 2.0 Pa·s at 25°C under their stated Brookfield conditions.
- Controlled mixing: Mix Part A and Part B at 100:45 by weight.
- Defined working window: Typical pot life is 30 minutes at 25°C for a 450 g mass.
- Room-temperature or accelerated cure: Cure for 5 to 7 days above 25°C, or use the supported small-mass accelerated schedule.
Suitable for
- Repair of metal aerospace structures
- Repair of composite aerospace structures
- Laminating and adhesive-injection repair processes
TDS, SDS & Technical Documents
Technical Specifications
General Properties
Physical Properties
Additional Information
LOCTITE EA 9323 AERO
This two-component, low-viscosity epoxy paste adhesive cures at room temperature for repair of metal and composite structures. Its unfilled formulation is used in laminating and injection processes, with supported lap-shear performance from -55°C to 177°C under the stated aluminum test configuration.

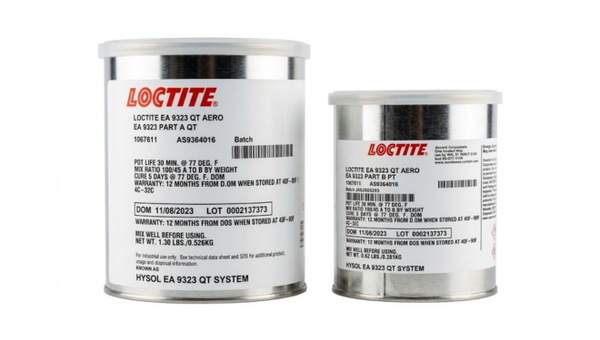
Two-part LOCTITE EA 9323 AERO adhesive system
As-Supplied Properties
Typical component properties and the required bulk-mixing ratio. Viscosity values apply to the separate components under the stated conditions.
| Property | Value | Unit | Method / condition |
|---|---|---|---|
| Product form | Two-component epoxy paste adhesive | — | Unfilled Part A and Part B system mixed immediately before application. |
| Color | Amber | — | Part A, Part B, and mixed adhesive. |
| Part A viscosity | 170 | Pa·s | 25°C; Brookfield HBT, spindle 5 at 10 rpm. |
| Part B viscosity | 2.0 | Pa·s | 25°C; equivalent to 20 Poise; Brookfield HBT, spindle 1 at 20 rpm. |
| Mix ratio, Part A:Part B | 100:45 | by weight | Volume measurement is not recommended for structural applications unless special precautions assure the correct ratio. |
Mixing, Application, and Cure
Bring the separate components close to room temperature, combine them at the required weight ratio, and mix completely before applying to clean, dry, prepared bonding surfaces. Control mixed mass and cure conditions to manage the working window and exotherm.
Recommended Processing Sequence
Store both components between 0°C and 25°C in tightly closed containers in a cool, well-ventilated area. At temperatures below 4°C, shelf life is 1 year for Part A and Part B. At temperatures below 25°C, shelf life is 3 months for Part A and 1 year for Part B. Place the material into its intended storage condition promptly after receipt.
Cured Material Properties
Typical bulk-resin and electrical properties. These values describe prepared test specimens and should not be treated as guaranteed design allowables for every bonded assembly.
| Property | Typical value | Unit | Method / condition |
|---|---|---|---|
| Service temperature | 121 | °C | Defined as the temperature at which the adhesive retains 6.9 MPa by ASTM D1002. |
| Tensile strength | 24.1 | MPa | 25°C; ASTM D638 using 3.18 mm castings. |
| Tensile modulus | 2.58 | GPa | 25°C; ASTM D638 using 3.18 mm castings. |
| Elongation at break | 9.0 | % | 25°C; ASTM D638 using 3.18 mm castings. |
| Shore D hardness | 84 | — | 25°C. |
| Glass transition temperature, dry | 97 | °C | Bulk-resin property. |
| Glass transition temperature, wet | 69 | °C | Bulk-resin property. |
| Shear modulus | 930 | MPa | Bulk-resin property. |
| Poisson's ratio | 0.39 | — | Bulk-resin property. |
| Compressive strength | 60.6 | MPa | 25°C; ASTM D695 using 12.7 mm castings. |
| Compressive modulus | 1.833 | GPa | 25°C; ASTM D695 using 12.7 mm castings. |
| Dielectric constant | 3.43 | — | 1 kHz at 25°C; electrical properties tested per ASTM D149/D150. |
| Dissipation factor | 0.017 | — | 1 kHz at 25°C; electrical properties tested per ASTM D149/D150. |
Bond Strength Performance
The following typical results preserve the tested substrates, surface preparations, cure, exposure, and test temperatures. Bond strength in another assembly depends on its materials, joint geometry, preparation, cure, and service conditions.
| Test temperature | Typical lap shear, MPa |
|---|---|
| -55°C | 19.3 |
| 25°C | 28.9 |
| 82°C | 8.3 |
| 121°C | 7.6 |
| 177°C | 4.1 |
| Exposure before test | Typical lap shear, MPa |
|---|---|
| Control | 28.9 |
| 49°C / 100% RH / 30 days | 19.3 |
| Salt spray at 41°C / 30 days | 21.7 |
| Test temperature | Typical peel strength, N/25 mm |
|---|---|
| -55°C | 22 |
| 25°C | 18 |
| 82°C | 98 |
Applications
LOCTITE EA 9323 AERO is used for repair work where its room-temperature cure, low component viscosity, and tested metal-bond performance align with the selected structure, preparation, and cure process.


Technical Support for LOCTITE EA 9323 AERO
Krayden can help review mix ratio, batch size, cure schedule, surface preparation, and the test conditions that matter for a metal or composite repair. Contact our technical team to discuss application fit and processing requirements for LOCTITE EA 9323 AERO.


