
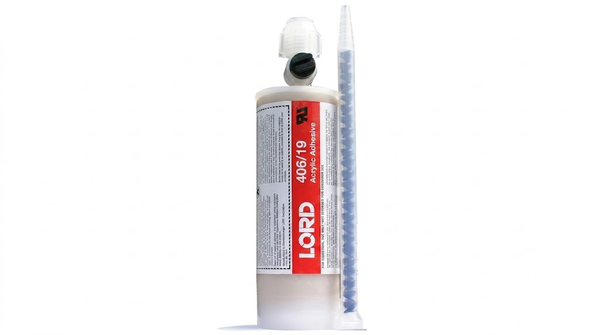
LORD 406/19GB
Harmonization Code : 8529.90 | Parts solely or principally used for TV, radio, and transmission
Main features
- 4:1 Metal-to-Plastic Bonding
- 6 to 10-Minute Working Window
- 18.6 MPa Cured Tensile Strength
Product Description
LORD® 406/19 Acrylic Adhesive is a two-component structural acrylic system consisting of LORD 406 adhesive and LORD Accelerator 19. Mixed at 4:1 by volume or approximately 3.02:1 by weight, the non-sag adhesive bonds many prepared or minimally prepared metals and engineered thermoplastics. It provides a typical 6–10 minute working time at 24°C, 12–17 minute handling-strength time, and 24-hour full cure. Typical cured properties include 18.6 MPa tensile strength, 30% elongation, 896 MPa Young’s modulus, and a 72°C glass-transition temperature.
Key features
- Dedicated LORD 406 adhesive and Accelerator 19 structural acrylic system
- Simple 4:1 volumetric mix ratio for cartridge or meter/mix processing
- Non-sag paste for vertical and overhead application
- High impact and peel performance, including low-temperature environments
- Accelerator 19 supports improved high-temperature resistance
- Room-temperature cure with handling strength in 12–17 minutes
- UL 746C positioning for the 406/19 system, subject to the current listed construction
Applications
- Bare, galvanised, stainless, and powder-coated metal assemblies
- Engineered thermoplastics including polycarbonate, ABS, acrylic, and validated blends
- Signs, enclosures, truck and trailer structures, and vehicle accessories
- Bonded assemblies that undergo a validated e-coat or powder-coat bake
Technical Specifications
General Properties
Thermal Properties
Physical Properties
Mechanical Properties
Additional Information
LORD® 406/19 Acrylic Adhesive
A dedicated two-component system combining LORD 406 adhesive with LORD Accelerator 19. The off-white-to-tan adhesive and off-white accelerator produce a tan mixed paste for structural bonding of metals and engineered plastics. Accelerator 19 is the selected cure component for improved high-temperature resistance and the system's published UL 746C positioning.

LORD 406 adhesive and Accelerator 19 at a controlled 4:1 ratio
| Property | LORD 406 adhesive | LORD Accelerator 19 | 406/19 mixed system |
|---|---|---|---|
| Appearance | Off-white to tan paste | Off-white paste | Tan paste |
| Viscosity at 25°C | 100,000–300,000 cP | 20,000–70,000 cP | No single mixed-viscosity value published |
| Density | 1090–1162 kg/m³ | 1467–1515 kg/m³ | Use component data and actual ratio for material calculations |
| Flash point | 15°C | >93°C | Follow both current SDS documents |
| Mix ratio | 4:1 adhesive-to-accelerator by volume; approximately 3.02:1 by weight | ||
| Solids content | 100% | ||
| Working time at 24°C | 6–10 minutes | ||
| Handling-strength time at 24°C | 12–17 minutes, based on the supplier's 60 psi shear criterion | ||
| Full cure at 24°C | 24 hours | ||
Prepare the substrate, purge the 4:1 cartridge, and apply before the working time expires
- Remove grease, loose contamination, and poorly adhering oxides from metals.
- Normal mill oils and drawing compounds may be tolerated, but actual production surfaces must be tested.
- Clean engineered plastics and abrade only where required for optimum adhesion.
- Level cartridge plungers before attaching the correct 4:1 mixer.
- Discard the initial purge until a uniform tan colour confirms proper mixing.
- Use handheld cartridges or automatic meter/mix/dispense equipment configured for 4:1 by volume.
- Apply and mate parts within the 6–10 minute working window.
- Use sufficient pressure for complete wet-out without starving the bondline.

Do not move or post-bake the assembly before handling strength
6–10 minutes at 24°C. Higher adhesive, substrate, or ambient temperature reduces available time.
12–17 minutes at 24°C under the TDS criterion. Fixture longer when joint load, mass, or geometry requires it.
24 hours at 24°C before using full cured-property data as the design basis.
The LORD acrylic family has documented powder-coat-bake capability, but the strongest 204°C/90-minute statement in DS3882 is specifically tied to LORD 406/19GB. Validate 406/19 separately.
Storage and industrial safety
LORD 406 is the flammable component of the 406/19 system and has a published 15°C flash point. The supplied EHS identifier was not available as a readable product-specific document. Confirm the current regional SDS for LORD 406 and LORD Accelerator 19 before publication or use. Follow both labels for ventilation, ignition control, personal protection, spill response, storage, transport, and disposal.
Published cured and joint data for LORD 406 with Accelerator 19
The values below are typical, not specification limits. Joint results remain tied to the stated substrate, surface condition, bondline, cure, specimen geometry, and test environment.
| Property or joint | Typical result | Context |
|---|---|---|
| Tensile strength at break | 18.6 MPa | Modified ASTM D638; 406/19. |
| Elongation | 30% | Modified ASTM D638. |
| Young’s modulus | 896.3 MPa | Modified ASTM D638. |
| Glass-transition temperature | 72°C | ASTM E1640 by DMA. |
| Aluminium lap shear, room temperature | 20.7 MPa | Cohesive failure reported. |
| Galvanised-steel lap shear, room temperature | 17.2 MPa | Cohesive failure reported. |
| Aluminium hot strength at 82°C | 10.3 MPa | Thin-layer cohesive failure reported. |
| Aluminium after 500 h salt spray | 18.3 MPa | Tested after 24 hours; thin-layer cohesive failure reported. |
| Aluminium after 14 days at 38°C/100% RH | 20.0 MPa | Cohesive failure reported. |
Use 406/19 where the accelerator choice, 4:1 equipment, and listed-system evidence match the assembly
LORD 406/19 is positioned for metals, engineered plastics, sign assemblies, enclosures, heavy-duty trucks, trailers, and vehicle accessories. The sign-industry application guide specifically identifies 406/19 for cold-rolled steel, aluminium, and stainless steel and references UL files E225855 and MH26317. Final qualification must address substrate lot and finish, thermal-expansion mismatch, joint geometry, bondline, impact, peel, corrosion, weathering, post-bake exposure, dimensional movement, and failure mode.
406/19 technical, processing, and application guidance
Controlling product-family TDS containing the 406/19 mix ratio, processing times, cured properties, bond data, and environmental results.
Open resourceCartridge levelling, mixer attachment, purging, bead application, mating, fixturing, cleanup, and storage guidance.
Open resourcePost-bake design guidance for LORD acrylic adhesive assemblies, including temporary softening and fixture support.
Open resourceJoint design, surface preparation, failure-mode, cartridge, bondline, fixturing, and rework guidance.
Open resourceGeneral product-selection and market-positioning guidance.
Open resourceProduct-specific sign-assembly context and UL file references for LORD 406/19.
Open resourceValidate the LORD® 406/19 system for your structural assembly
Krayden can help review substrate preparation, 4:1 package and equipment configuration, static mixer, purge, bead size, work time, fixturing, bondline control, UL construction, environmental exposure, powder-coat processing, and final assembly qualification.


